English

English

Get a Quote
News
  • Should You Use a Ball Valve for Throttling? Seat Damage, Cavitation and Better Alternatives
    Should You Use a Ball Valve for Throttling? Seat Damage, Cavitation and Better Alternatives Nov 05, 2026
    A standard on-off ball valve should not be the default choice for continuous throttling. It can restrict flow, but that does not make it a control valve. Holding it partly open can expose the seat to a concentrated high-velocity jet, produce unstable control and, in liquid service, create cavitation. Brief restriction during start-up or shutdown may be acceptable if the manufacturer permits it. Regular modulation requires a valve designed and sized for that duty.   A Part-Open Ball Puts the Seat in the Flow Path   When a standard ball valve is fully open, the bore provides a relatively straight flow path. As the ball rotates toward closed, the opening becomes a narrow, changing shape. Velocity rises through this restriction, and the emerging jet can pass close to the downstream seat edge and body cavity.   That matters because the seat performs the shutoff function. A soft seat may deform, cut or erode under high velocity, heat and entrained solids. A metal seat may tolerate harsher conditions, but hardness alone does not provide a suitable control characteristic or prevent local erosion. Damage often appears later as increased shutoff leakage, even though the valve still moves normally.   Control quality is another limitation. A conventional full-port ball may pass a large increase in flow over a small change in travel once it begins to open. The actuator can therefore hunt around a narrow angle instead of positioning smoothly across a useful range. A positioner cannot correct an unsuitable valve characteristic.   Cavitation Depends on the Local Pressure, Not Just Line Pressure   Cavitation is possible when liquid accelerates through the restriction and its local pressure falls below the liquid's vapour pressure. Vapour bubbles then form. If pressure recovers above vapour pressure downstream, the bubbles collapse and release damaging energy near the valve or downstream pipe.   Ball valves are generally high-recovery valves: much of the pressure lost at the narrowest flow area is recovered downstream. That means the minimum internal pressure can be considerably lower than the measured outlet pressure. A moderate-looking inlet-to-outlet pressure drop may therefore hide a more severe pressure dip inside the valve.   Noise resembling gravel, vibration and rough pitting are warning signs, but sound alone is not a design method. The evaluation needs minimum, normal and maximum flow; upstream and downstream pressure at each case; fluid temperature and vapour pressure; density; solids content; valve size; and the manufacturer's pressure-recovery and sizing data. If downstream pressure remains below vapour pressure, the condition is flashing rather than cavitation and requires a different damage assessment.     A Ball Valve Can Throttle When It Is a Control Valve   A V-port or segmented ball introduces a shaped opening that gives a more predictable relationship between travel and flow. Correctly sele...
    View More
  • What Keeps a Gate Valve from Opening After Shutdown: Pressure Locking or Thermal Binding?
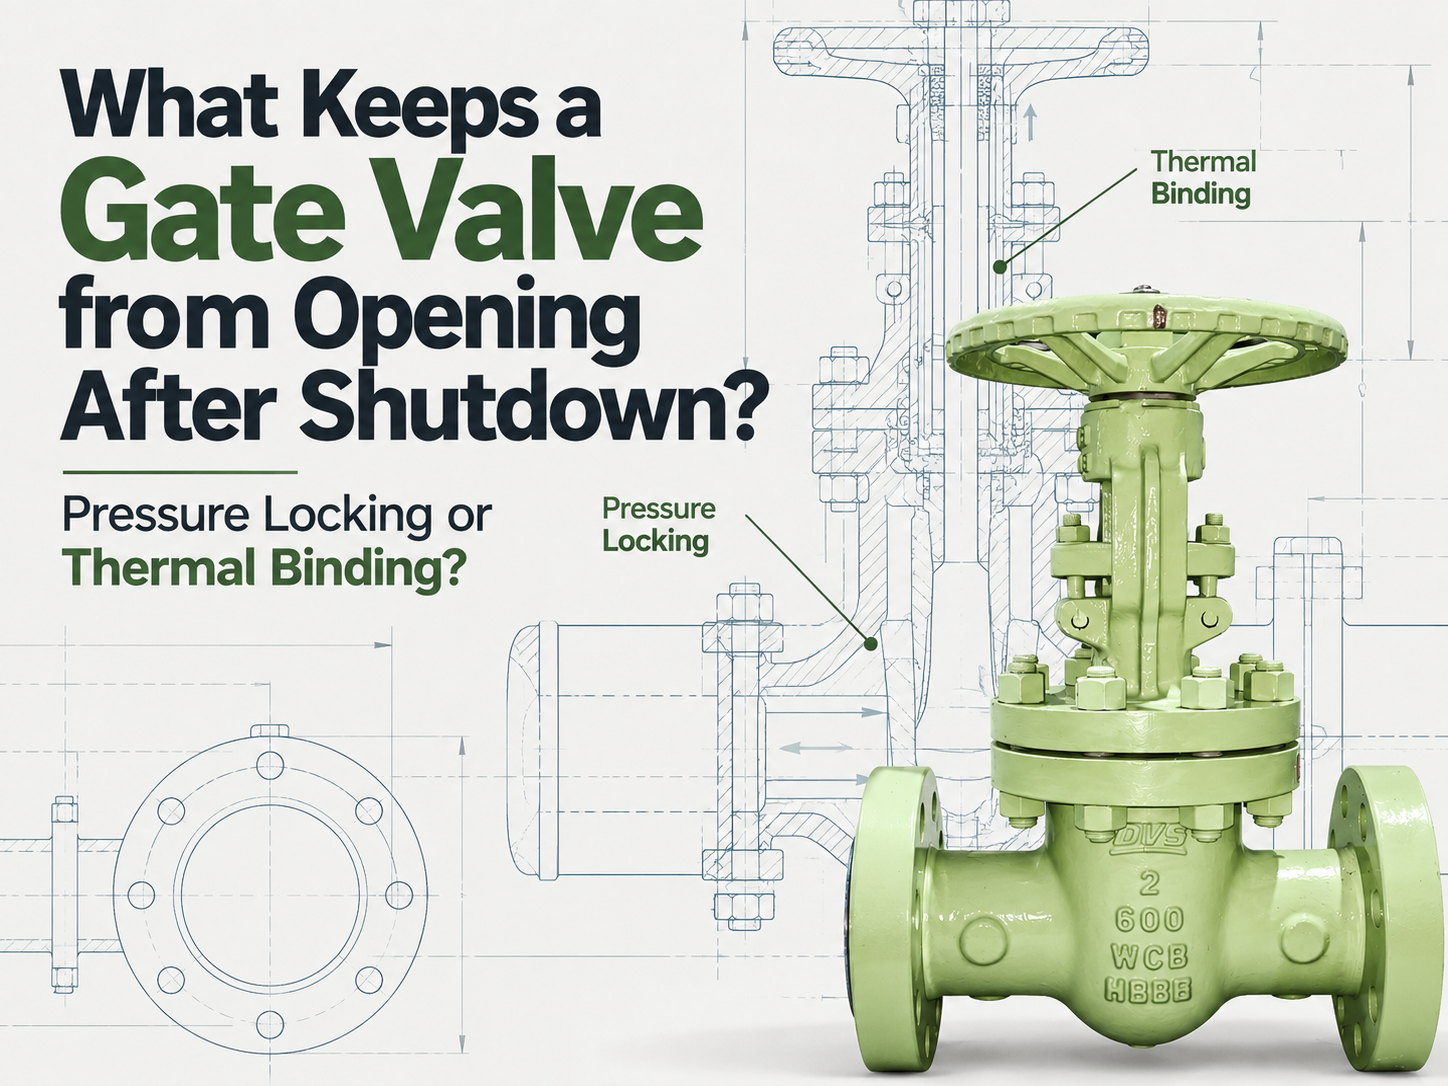
    What Keeps a Gate Valve from Opening After Shutdown: Pressure Locking or Thermal Binding? Oct 30, 2026
    A gate valve that will not open after shutdown may be pressure locked or thermally bound, and the shutdown history usually separates the two. Pressure locking means pressure is trapped in the bonnet cavity; thermal binding means a hot-closed wedge has developed mechanical interference during cooldown. Neither is an automatic reason to raise the actuator torque setting.   Pressure Locking Starts in the Bonnet Cavity   Pressure locking can affect flexible-wedge and double-disc gate valves when liquid enters the bonnet cavity during operation or through slight seat movement or leakage. Once the valve is closed, that liquid may be trapped between the two seating boundaries.   The problem develops when cavity pressure exceeds the pressure on both sides of the closed gate. The line may have been depressurised after the cavity filled at operating pressure, or trapped liquid may have heated and expanded. The resulting load forces the closure element against both seats, leaving normal actuator thrust insufficient to start opening.   A failed opening after line depressurisation, or after the closed valve was heated, points toward pressure locking. Where an approved connection permits measurement, bonnet pressure is stronger evidence than high motor current or a torque trip alone.   Thermal Binding Follows Hot Closure and Cooldown   Thermal binding follows a different sequence. A wedge gate valve is seated hot and the system cools before the next opening command. Unequal contraction of the body and wedge can increase mechanical interference at the seats. Solid wedges are particularly susceptible, although large temperature changes can also affect flexible wedges.   This mechanism does not require an overpressurised cavity. Its strongest clue is timing: the valve closes normally at operating temperature but refuses to open after cooldown. Behaviour that changes as temperature returns toward the closing condition supports the diagnosis, but deliberate reheating requires an approved procedure. Uncontrolled external heating is unsafe.   Reconstruct the Shutdown Before Touching the Torque Switch   Start with the pressure and temperature timeline. Record when the valve closed, whether either side was later drained or depressurised, whether the body remained exposed to heat, and the temperature at the failed opening attempt. Confirm the gate design from drawings or manufacturer records; solid-wedge, flexible-wedge and double-disc designs do not share the same susceptibility.   Rule out ordinary faults such as lost power or pressure, wrong limit or torque-switch settings, stem or packing friction, gearbox damage, corrosion and debris. Actuator alarms and the point where movement stopped help distinguish a drive problem from a gate held at the seats.   Do not bypass the torque switch or repeatedly hammer the valve open. Extra thrust may bend the stem, damage the seats or overload the gearbox. A larger actuator d...
    View More
  • Top 10 Industrial Valve Manufacturers in China for 2026: How to Choose the Right Supplier
    Top 10 Industrial Valve Manufacturers in China for 2026: How to Choose the Right Supplier Oct 22, 2026
    1. Suzhou Neway Valve Co., Ltd. — NEWAY NEWAY is one of China's most internationally recognized industrial valve manufacturers. Its product range includes ball valves, gate valves, globe valves, check valves, butterfly valves, cryogenic valves, subsea valves, and other engineered valve solutions. The company has strong experience in oil and gas, LNG, petrochemical, offshore, and power applications.   Best suited for: large-scale energy projects and severe-service applications. 2. CNNC Sufa Technology Industry Co., Ltd. CNNC SUFA is well known for its experience in nuclear power and other high-integrity industrial applications. The company has strong capabilities in material traceability, engineering control, testing, and specialized valve manufacturing. Its products are also used in petroleum, petrochemical, power, and chemical industries.   Best suited for: nuclear power, high-integrity systems, and technically demanding projects. 3. DERVOS VALVE DERVOS VALVE supplies industrial valves to customers in oil and gas, petrochemical, power generation, water treatment, marine, and general industrial applications. Its main products include ball valves, gate valves, globe valves, check valves, butterfly valves, plug valves, knife gate valves, line blind valves, and strainers. DERVOS supports international standards such as API, ASME, EN, and DIN, and can provide carbon steel, stainless steel, alloy steel, duplex stainless steel, low-temperature steel, and other materials. One of its key strengths is flexibility. DERVOS can support mixed valve packages, small-to-medium quantities, customized specifications, and project-specific documentation.   Best suited for: overseas distributors, EPC projects, customized valves, mixed orders, and flexible sourcing requirements.   4. Yuanda Valve Group Yuanda Valve Group is one of China's large-scale valve manufacturers with broad production capacity. Its product range includes gate valves, globe valves, check valves, butterfly valves, ball valves, and other general industrial valves. The company is widely involved in water supply, HVAC, municipal infrastructure, power, and industrial pipeline projects. Best suited for: large-volume standardized valve procurement and general industrial applications.   5. Jiangsu Shentong Valve Co., Ltd. Jiangsu Shentong focuses strongly on specialized valve applications in metallurgy, energy, nuclear power, and chemical industries. Its strength lies in engineered products for demanding operating conditions rather than only standard valve production. Best suited for: metallurgy, energy, chemical processing, and specialized industrial applications.   6. Chaoda Valves Group Co., Ltd. Chaoda Valves Group serves petroleum, chemical, natural gas, power, and other process industries. Its product range includes ball valves, gate valves, globe valves, check valves, butterfly valves, and special-purpose industrial valves. The company has experience with corro...
    View More
  • Why Does a Check Valve Slam After Pump Shutdown? Causes and Non-Slam Design Options
    Why Does a Check Valve Slam After Pump Shutdown? Causes and Non-Slam Design Options Oct 22, 2026
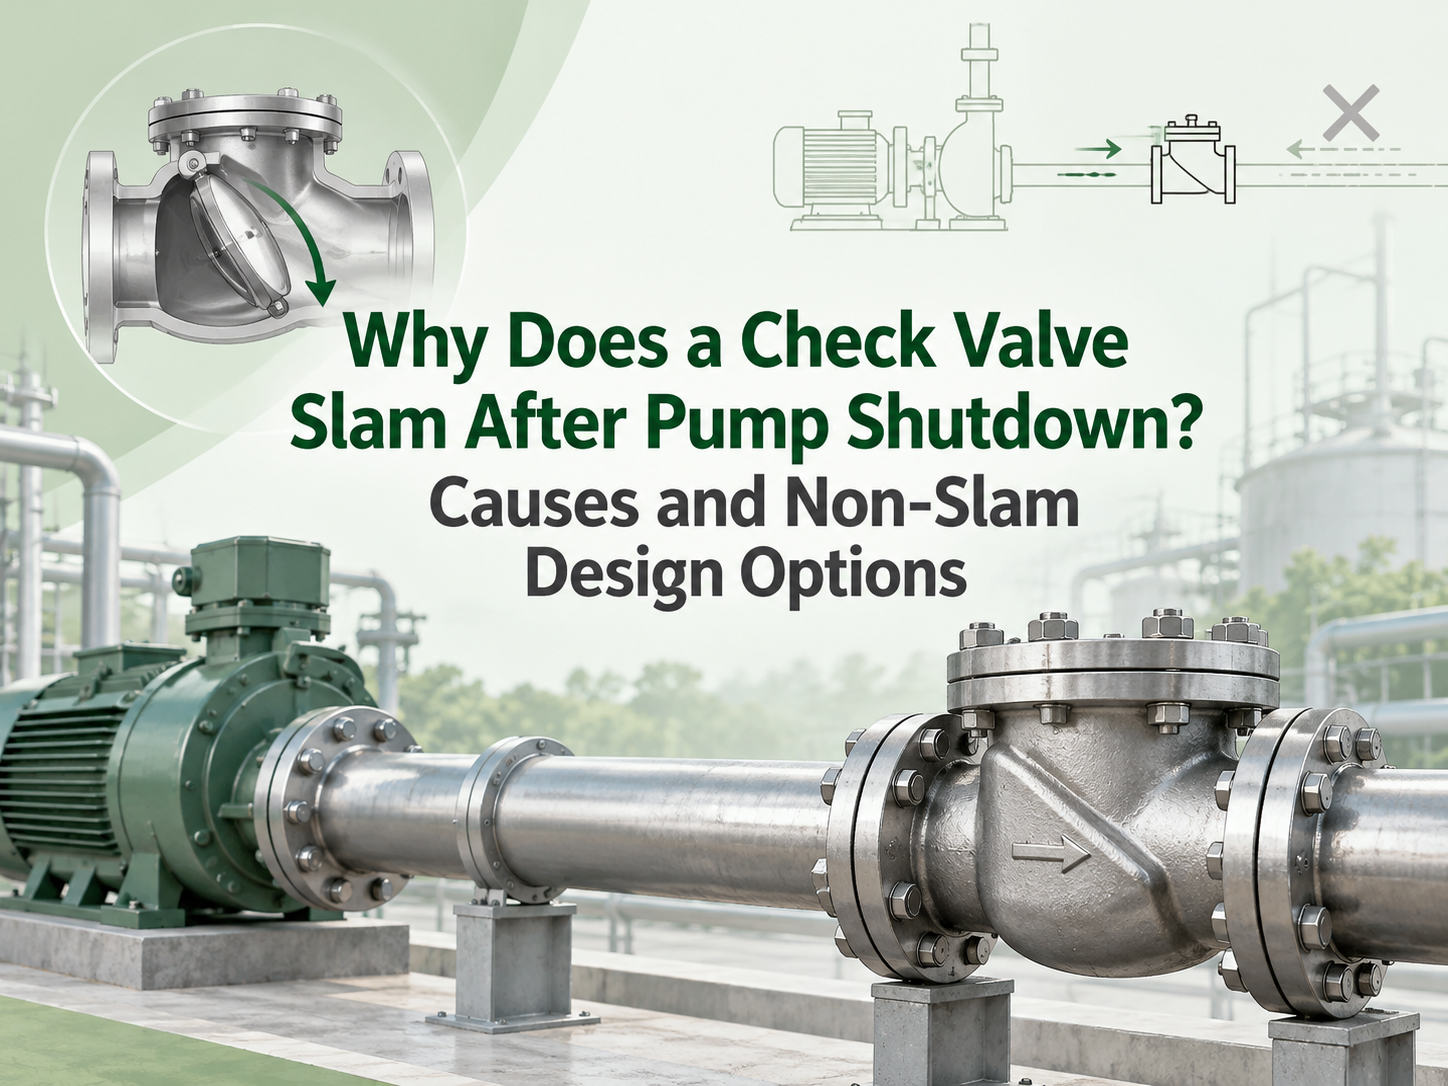
    A check valve slams after pump shutdown when flow reverses before the closure member reaches its seat. The valve then stops that reverse velocity abruptly, creating a pressure wave through the piping. The damaging event is usually the rapid arrest of the liquid column, not simply the disc hitting the seat. A “non-slam” label alone is not a solution; the valve response must suit the system's flow deceleration.   The Valve Is Closing Too Late for the Shutdown Transient   When pump torque disappears, forward velocity falls. Static head, a pressurised common header or another running pump may then drive liquid back toward the stopped pump. If inertia and hinge friction keep a conventional swing disc open through zero flow, reverse velocity develops before the disc reaches its seat.   High static lift, a steep rising main, short pump coast-down, parallel pumps and high initial velocity can accelerate this reversal. A long-stroke or high-inertia valve is more likely to lag. This is why the same valve may run quietly in one system and slam in another: nominal size and pressure class do not define shutdown behaviour.   Confirm the Event Before Changing the Valve   A single hard bang after shutdown points toward check-valve closure or another surge event. Continuous clicking during forward flow is chatter, which more often indicates unstable partial opening, pulsation or poor hydraulic sizing.   Record the stop command, motor speed decay, flow direction and pressures on both sides of the valve on a common time base. A high-speed video of an external lever or position indicator can help show when the valve closes. For consequential systems, fast pressure logging is more reliable than sound alone.   Inspect the hinge, shaft, spring and seat for friction, wear, deposits or damage, and verify the permitted installation orientation. Check pipe supports as well; the pressure wave may produce its loudest noise away from the valve.   Non-Slam Designs Use Different Closing Strategies   An axial-flow or nozzle check valve uses a light, centrally guided disc, short travel and spring assistance. It begins closing as forward flow falls, ideally seating before appreciable reversal. It is a strong candidate for rapid pump trips, but pressure loss, cracking pressure, minimum stable flow, orientation and tolerance of solids still matter.   A spring-assisted dual-plate valve uses two lighter plates and shorter travel than a conventional swing disc. Its compact construction can improve response, but “dual plate” does not mean slam-free. Plate inertia, spring torque, size and mounting position remain relevant.   Tilting-disc, resilient-hinge and spring-assisted swing designs reduce travel or assist closure while retaining a relatively open flow path. They can suit large water lines where energy loss matters, provided dynamic data supports the selected design and size.   Large pumping mains ma...
    View More
  • Will a Line Blind Spill Product During Changeover? Open vs Non-Spill vs Enclosed Designs
    Will a Line Blind Spill Product During Changeover? Open vs Non-Spill vs Enclosed Designs Oct 16, 2026
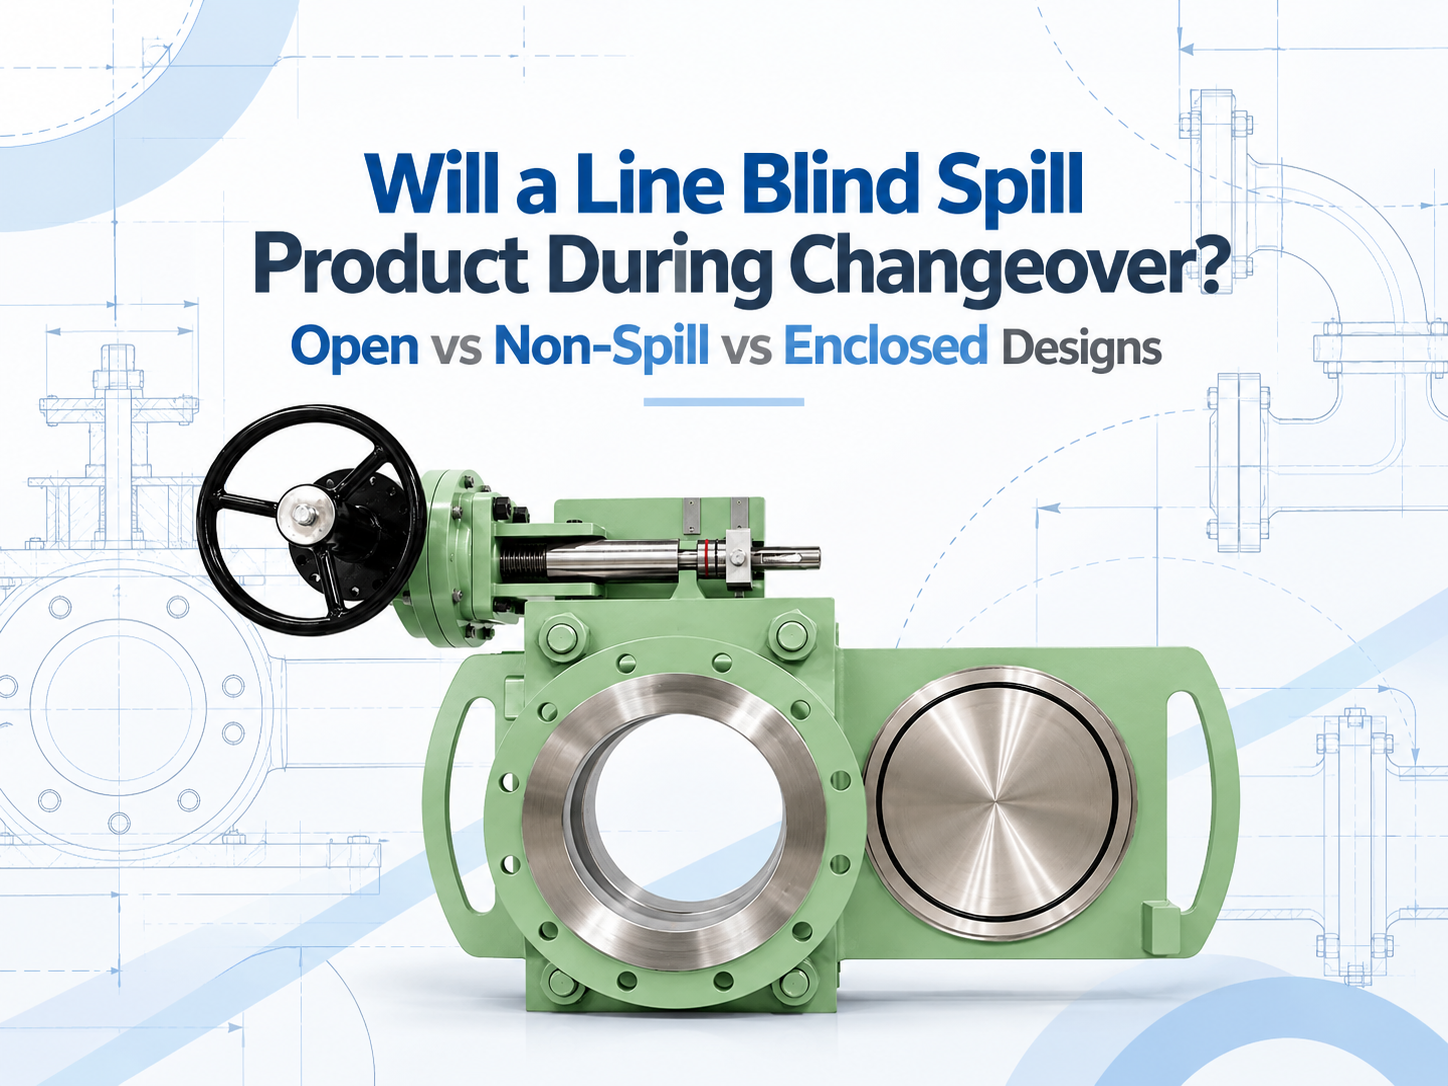
    Yes, an open-body line blind can release residual product when it changes between the open and blind positions. A non-spill design does not make that residue disappear; it catches the liquid in a partial enclosure and directs it to a drain. An enclosed design can provide better control of liquid and vapour, but only when its housing, drain, vent and purge connections are engineered for the service. None of these labels should be read as permission to move the blind under live line pressure.   Why Product Can Escape During Changeover   When a line blind is fully clamped, its seals contain the process and the solid plate provides positive isolation in the blind position. Changeover is different. The sealing faces must separate before the spectacle or sliding plate can move. During that interval, the body cavity and plate path may be open to the surrounding area.   The line should already be isolated, depressurised and drained, but “drained” rarely means perfectly dry. Liquid can remain as a film on the plate, collect in the lower body, or sit in a poorly drained pipe pocket. Gas service may leave flammable, toxic or odorous vapour. The amount released therefore depends as much on piping layout and the shutdown procedure as on the line blind itself.   The Three Designs Manage Residue Differently   Open-body design   Residual liquid can drip from the exposed plate path into a temporary tray or the work area, while vapour disperses locally. This arrangement can suit water, steam condensate or other manageable media where easy access and visual inspection matter. It presents the highest potential for floor contamination and operator exposure.   Non-spill design   A bottom-and-side cover catches drips and sends them to a drain or recovery container; the top may remain open. This design is commonly considered for fuel terminals, marine service and liquid duties where ground or deck contamination must be controlled. It reduces dripping but may not contain vapour, and a blocked drain defeats its purpose.   Enclosed design   A housing surrounds more or all of the plate travel and may connect to a closed drain, purge, vent, flare or vapour-recovery system. It is better suited to toxic, flammable, odorous or environmentally sensitive service requiring controlled containment. The tradeoff is greater complexity in purging, inspection and maintenance, together with the need to manage trapped pressure deliberately.   These names are not perfectly standardised across manufacturers. One supplier's “non-spill” model may be open at the top, while another product described as enclosed may use a more complete casing. The RFQ should show the enclosure arrangement and identify every opening rather than relying on the product name.   Non-Spill Does Not Automatically Mean Zero Release   For a liquid with low volatility, catching the remaining drops and routing them into a closed contai...
    View More
  • How Often Do You Open the Pipeline? When Is a Line Blind Valve Worth Installing?
    How Often Do You Open the Pipeline? When Is a Line Blind Valve Worth Installing? Sep 30, 2026
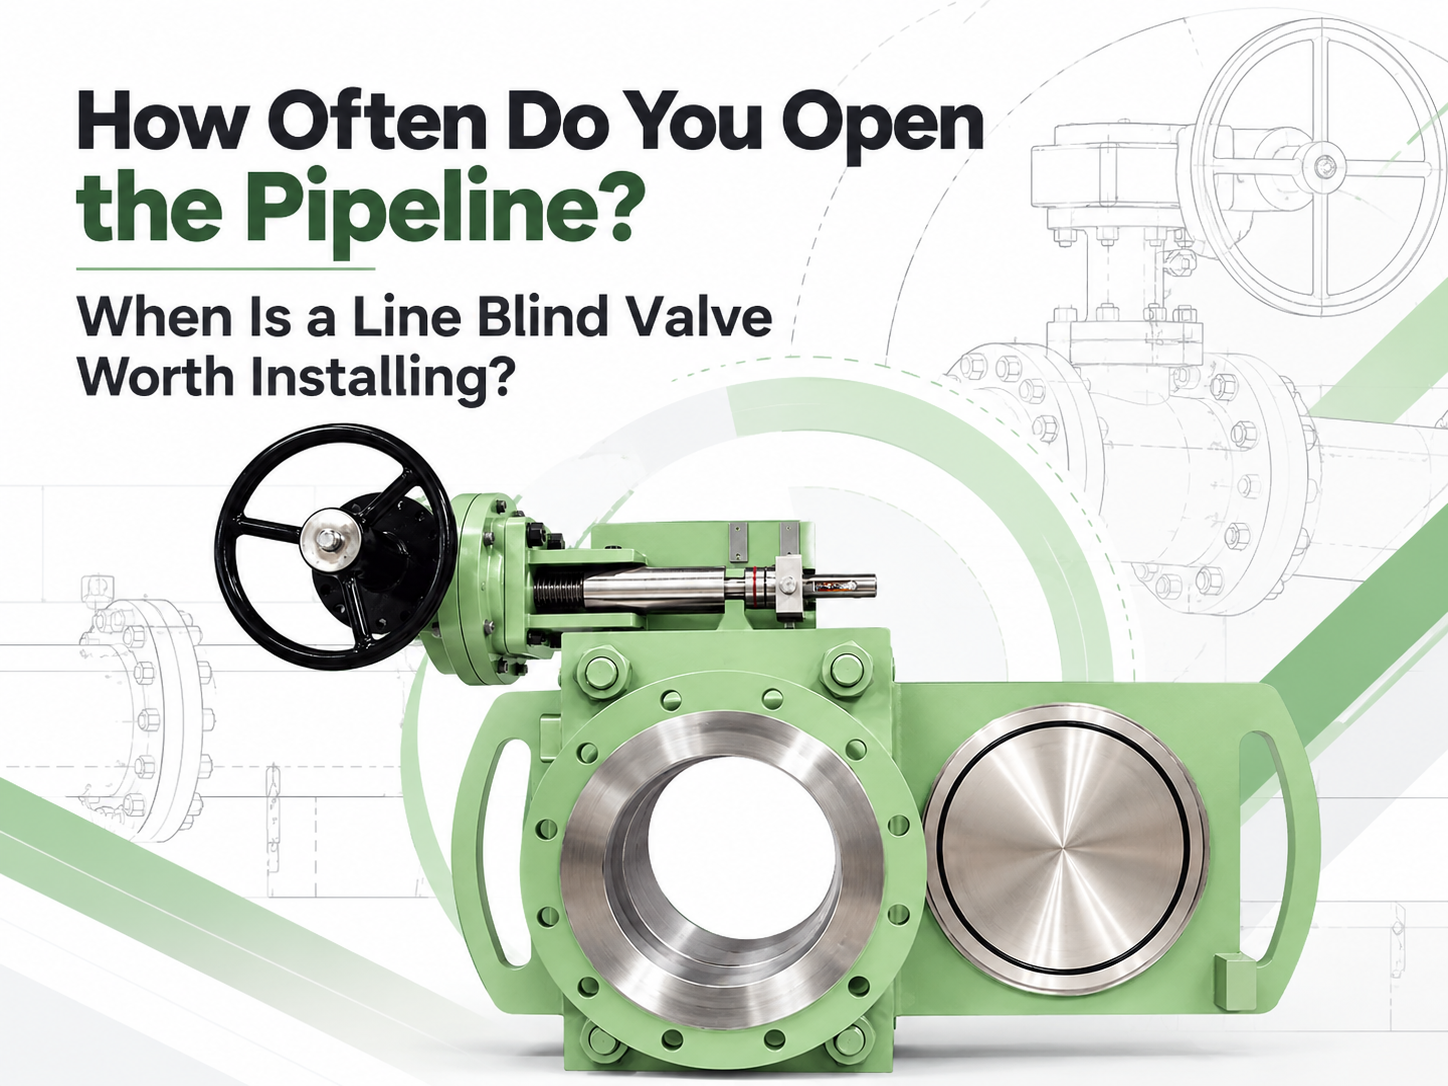
    A line blind valve is worth evaluating when a pipeline is blinded several times a year, or when one conventional changeover causes hours of shutdown, lifting work or significant exposure to hazardous residue. No universal cycle count guarantees payback. A large critical line operated twice a year may justify the investment, while a small accessible line operated monthly may not.   The decision should be based on the cost and risk of each complete isolation event, not frequency alone.   There Is No Standard “Two Operations per Year” Rule   Some suppliers use one or two annual changeovers as a screening threshold. That can start a discussion, but it is not an engineering rule. Frequency has very different consequences on a DN50 utility line and a DN600 process-gas main.   For a preliminary review, the following bands are useful but not mandatory: Blinding frequency  Initial interpretation Once per major turnaround or less A removable blind or spectacle blind is often more economical. One to three times per year Compare labor, lifting, outage duration and medium risk carefully. Quarterly to monthly A quick-action line blind is normally a strong candidate. Weekly or more often Purpose-built or automated isolation deserves detailed review; also confirm that a line blind is suitable for the required cycle duty.   A low operating frequency can still support installation when every event requires scaffolding, a crane, several pipefitters or a long production interruption. Conversely, frequent operation does not justify a line blind if the process cannot accommodate its pressure, temperature, materials or maintenance needs.   Count the Complete Changeover   Traditional blinding is more than moving a plate. After the line is made safe, workers loosen bolting, spread the flange joint, handle the blind or spacer, replace gaskets, restore alignment, tighten the joint and complete leak checks. Large sizes add rigging and access equipment.   A quick-action line blind keeps the spectacle or sliding plate supported inside the installed assembly. Manufacturer literature commonly reports one-person changeover in minutes rather than the man-hours needed for conventional flange work. Those figures are useful for screening, but the project calculation should use the plant’s own procedures and recorded shutdown times.   Use a simple comparison: Annual avoided cost = operations per year x cost avoided per operation   Avoided cost may include pipefitter hours, rigging, scaffolding, gaskets and bolting, leak testing and the production value of saved time. Keep categories separate to avoid double counting. Compare the annual saving with the line blind’s additional installed price and maintenance cost.   Risk Can Matter More Than Simple Payback   Repeated flange separation creates opportunities for residual-medium exposure, damaged flange faces, poor alignment and inconsistent bolt load...
    View More
first page 1 2 3 4 5 6 7 8 9 10 last page
[  A total of  52  pages]

Leave a message

    If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.

Home

Products

about

contact