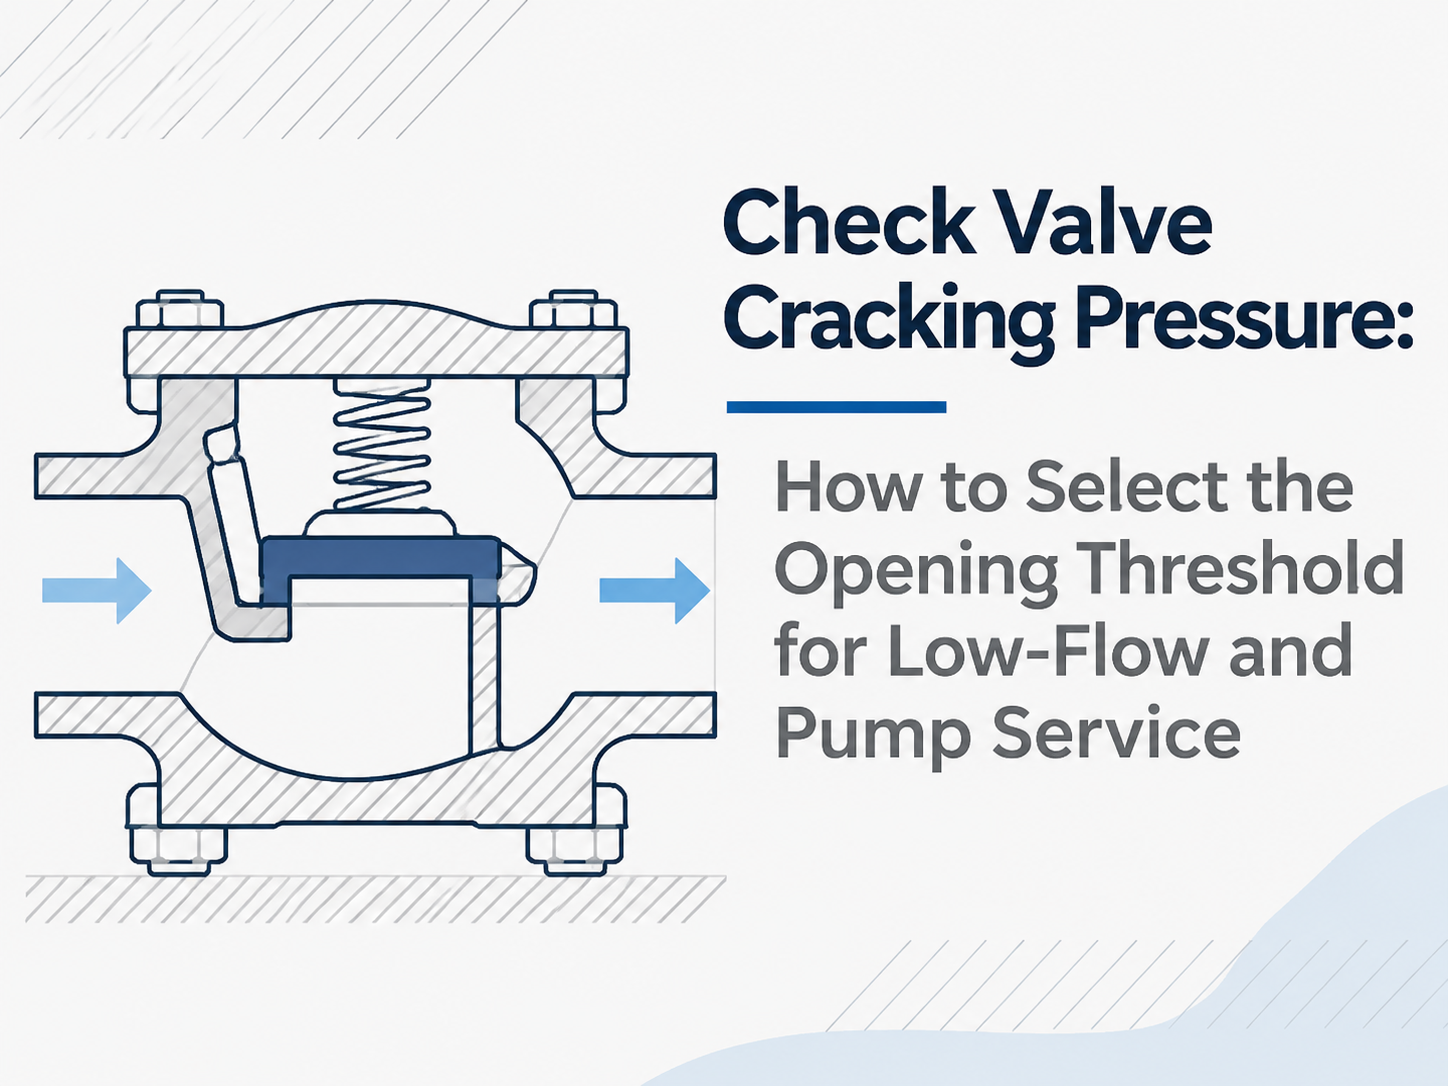
A check valve can begin to pass fluid and still be far from a stable open position. Check valve cracking pressure is therefore the threshold for first detectable flow, not the full-open pressure drop or proof of reliable minimum-flow operation. For low-flow and pump service, the opening threshold is acceptable only when the system can exceed it in the worst forward-flow case. The selection must then pass three separate checks: stable valve travel at minimum flow, acceptable pressure loss at normal and maximum flow, and timely closure when the pump stops. Start with the Worst Available Differential Pressure Parker defines cracking pressure as the upstream pressure at which detectable flow is measured, while Swagelok notes that first flow does not mean the valve is fully open. The relevant system value is not pump discharge pressure alone, but the pressure difference across the valve when it must open. For an initial screen: Available opening ΔP = minimum upstream pressure at the valve − maximum downstream pressure at the valve If the pressures come from remote points, correct them for elevation and line losses. Evaluate the least favorable credible case, such as a variable-speed pump starting at low speed or a standby pump opening against a live common header. The maximum guaranteed cracking pressure of the offered valve should be below this available ΔP, with an engineering allowance for manufacturing tolerance, temperature, orientation, deposits and measurement uncertainty. There is no defensible universal allowance. A nominal value alone is insufficient because catalog cracking pressure may be specified as a range, and a valve left idle may initially require a higher differential than it does after cycling. Low Cracking Pressure Does Not Solve Low-Flow Instability After the closure member lifts, more differential pressure and flow force are needed for stable travel. An oversized valve may crack open but hover near the seat because velocity is too low, causing clicking, flutter, impact and accelerated wear. Swagelok’s service guidance identifies excessive spring cracking pressure and excessive valve size as possible causes of chatter near the threshold. Size from the operating envelope rather than automatically matching the pipe diameter. Ask the supplier to evaluate three points for the exact size, spring and trim: Operating point Required evidence Minimum continuous flow Stable-open position, minimum stable flow or velocity, and corresponding ΔP Normal flow Model-specific pressure-drop curve or validated flow coefficient Maximum flow Peak ΔP, velocity limits, erosion risk and acceptable travel Cracking pressure answers “When does motion begin?” The flow curve and stable-flow limit answer “Will the valve remain open without damaging itself?” Pump Opening and Pump Shutdown Are Different Design Cases At s...
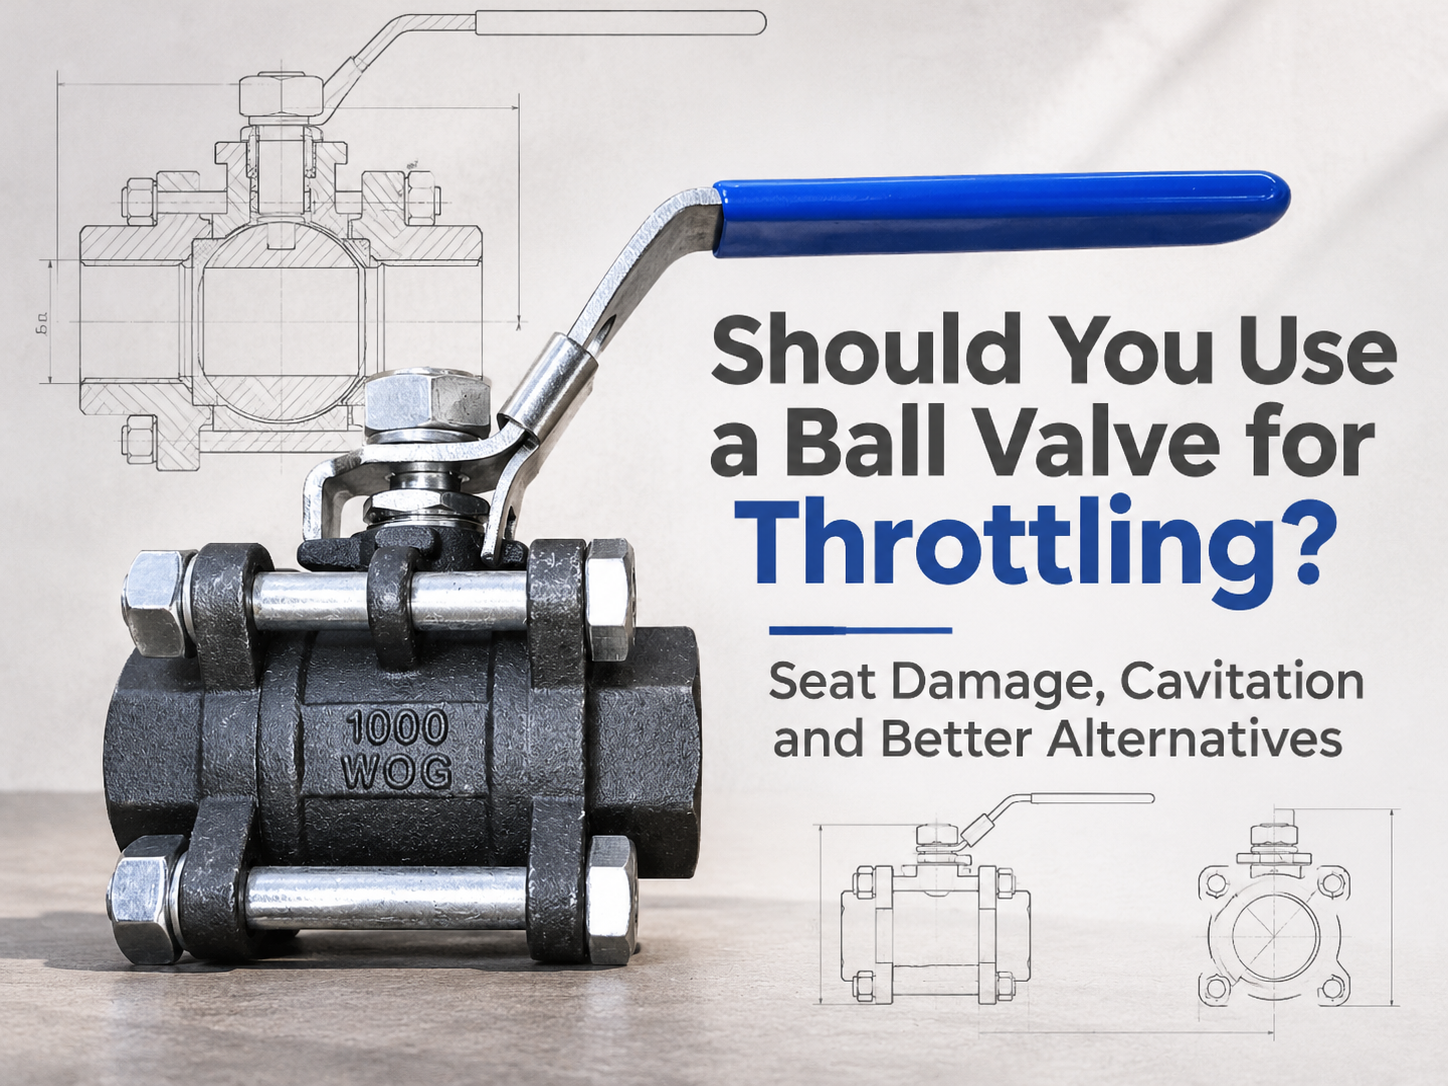
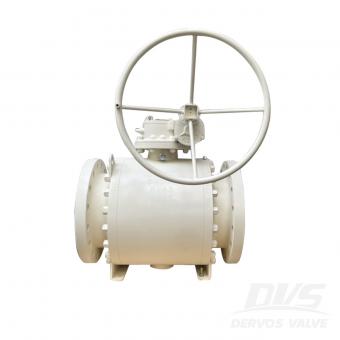
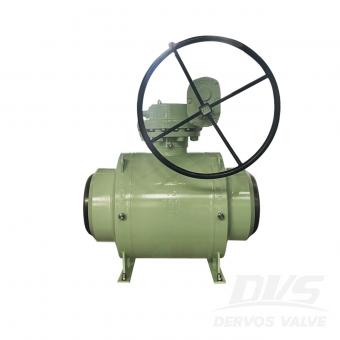
A standard on-off ball valve should not be the default choice for continuous throttling. It can restrict flow, but that does not make it a control valve. Holding it partly open can expose the seat to a concentrated high-velocity jet, produce unstable control and, in liquid service, create cavitation. Brief restriction during start-up or shutdown may be acceptable if the manufacturer permits it. Regular modulation requires a valve designed and sized for that duty. A Part-Open Ball Puts the Seat in the Flow Path When a standard ball valve is fully open, the bore provides a relatively straight flow path. As the ball rotates toward closed, the opening becomes a narrow, changing shape. Velocity rises through this restriction, and the emerging jet can pass close to the downstream seat edge and body cavity. That matters because the seat performs the shutoff function. A soft seat may deform, cut or erode under high velocity, heat and entrained solids. A metal seat may tolerate harsher conditions, but hardness alone does not provide a suitable control characteristic or prevent local erosion. Damage often appears later as increased shutoff leakage, even though the valve still moves normally. Control quality is another limitation. A conventional full-port ball may pass a large increase in flow over a small change in travel once it begins to open. The actuator can therefore hunt around a narrow angle instead of positioning smoothly across a useful range. A positioner cannot correct an unsuitable valve characteristic. Cavitation Depends on the Local Pressure, Not Just Line Pressure Cavitation is possible when liquid accelerates through the restriction and its local pressure falls below the liquid's vapour pressure. Vapour bubbles then form. If pressure recovers above vapour pressure downstream, the bubbles collapse and release damaging energy near the valve or downstream pipe. Ball valves are generally high-recovery valves: much of the pressure lost at the narrowest flow area is recovered downstream. That means the minimum internal pressure can be considerably lower than the measured outlet pressure. A moderate-looking inlet-to-outlet pressure drop may therefore hide a more severe pressure dip inside the valve. Noise resembling gravel, vibration and rough pitting are warning signs, but sound alone is not a design method. The evaluation needs minimum, normal and maximum flow; upstream and downstream pressure at each case; fluid temperature and vapour pressure; density; solids content; valve size; and the manufacturer's pressure-recovery and sizing data. If downstream pressure remains below vapour pressure, the condition is flashing rather than cavitation and requires a different damage assessment. A Ball Valve Can Throttle When It Is a Control Valve A V-port or segmented ball introduces a shaped opening that gives a more predictable relationship between travel and flow. Correctly sele...
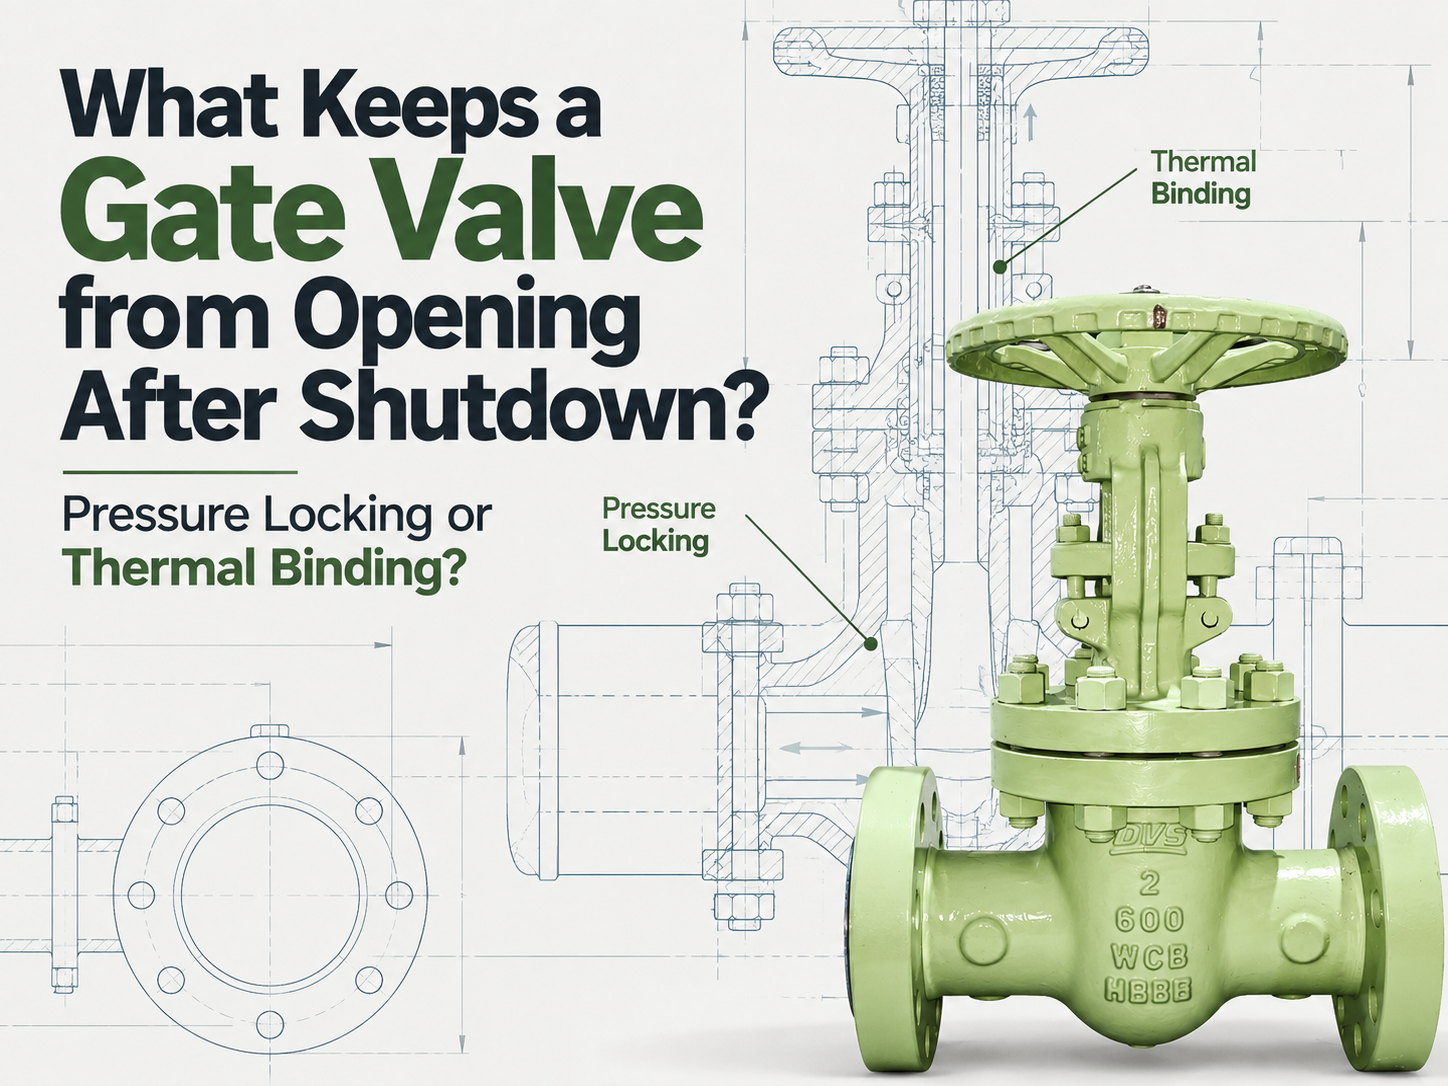
A gate valve that will not open after shutdown may be pressure locked or thermally bound, and the shutdown history usually separates the two. Pressure locking means pressure is trapped in the bonnet cavity; thermal binding means a hot-closed wedge has developed mechanical interference during cooldown. Neither is an automatic reason to raise the actuator torque setting. Pressure Locking Starts in the Bonnet Cavity Pressure locking can affect flexible-wedge and double-disc gate valves when liquid enters the bonnet cavity during operation or through slight seat movement or leakage. Once the valve is closed, that liquid may be trapped between the two seating boundaries. The problem develops when cavity pressure exceeds the pressure on both sides of the closed gate. The line may have been depressurised after the cavity filled at operating pressure, or trapped liquid may have heated and expanded. The resulting load forces the closure element against both seats, leaving normal actuator thrust insufficient to start opening. A failed opening after line depressurisation, or after the closed valve was heated, points toward pressure locking. Where an approved connection permits measurement, bonnet pressure is stronger evidence than high motor current or a torque trip alone. Thermal Binding Follows Hot Closure and Cooldown Thermal binding follows a different sequence. A wedge gate valve is seated hot and the system cools before the next opening command. Unequal contraction of the body and wedge can increase mechanical interference at the seats. Solid wedges are particularly susceptible, although large temperature changes can also affect flexible wedges. This mechanism does not require an overpressurised cavity. Its strongest clue is timing: the valve closes normally at operating temperature but refuses to open after cooldown. Behaviour that changes as temperature returns toward the closing condition supports the diagnosis, but deliberate reheating requires an approved procedure. Uncontrolled external heating is unsafe. Reconstruct the Shutdown Before Touching the Torque Switch Start with the pressure and temperature timeline. Record when the valve closed, whether either side was later drained or depressurised, whether the body remained exposed to heat, and the temperature at the failed opening attempt. Confirm the gate design from drawings or manufacturer records; solid-wedge, flexible-wedge and double-disc designs do not share the same susceptibility. Rule out ordinary faults such as lost power or pressure, wrong limit or torque-switch settings, stem or packing friction, gearbox damage, corrosion and debris. Actuator alarms and the point where movement stopped help distinguish a drive problem from a gate held at the seats. Do not bypass the torque switch or repeatedly hammer the valve open. Extra thrust may bend the stem, damage the seats or overload the gearbox. A larger actuator d...
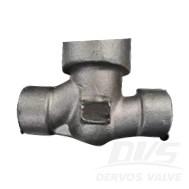
1" 2500LB check valve is made according to ASME B16.34 standard. The valve body is made of F316L. It has the structural characteristics of lifting type, pressure self-sealing, conventional diameter. Its connection mode is FNPT.
Payment:
30% when order confirmed, 70% before shipmentProduct Origin:
ChinaColor:
CustomizationShipping Port:
Shanghai, ChinaLead Time:
30~60 days Ex Works after order confirmationMaterial:
A182 F316LProduct Description
|
Type |
Lift Check Valve |
|
Size |
1" |
|
Pressure |
2500LB |
|
Connection |
FNPT |
|
Body Material |
A182 F316L |
|
Design Norm |
ASME B16.34 |
|
Screwed Ends Dimension |
ASME B1.20.1 |
|
Test & Inspection Code |
API 598 |
|
Temperature |
-29 ~ 38°C |
|
Applicable Medium |
Water, Oil and Gas |
Features
1. Clean the valve before installation and eliminate the defects caused during transportation;
2. Do not load the check valve in the pipeline.
Technical Drawing
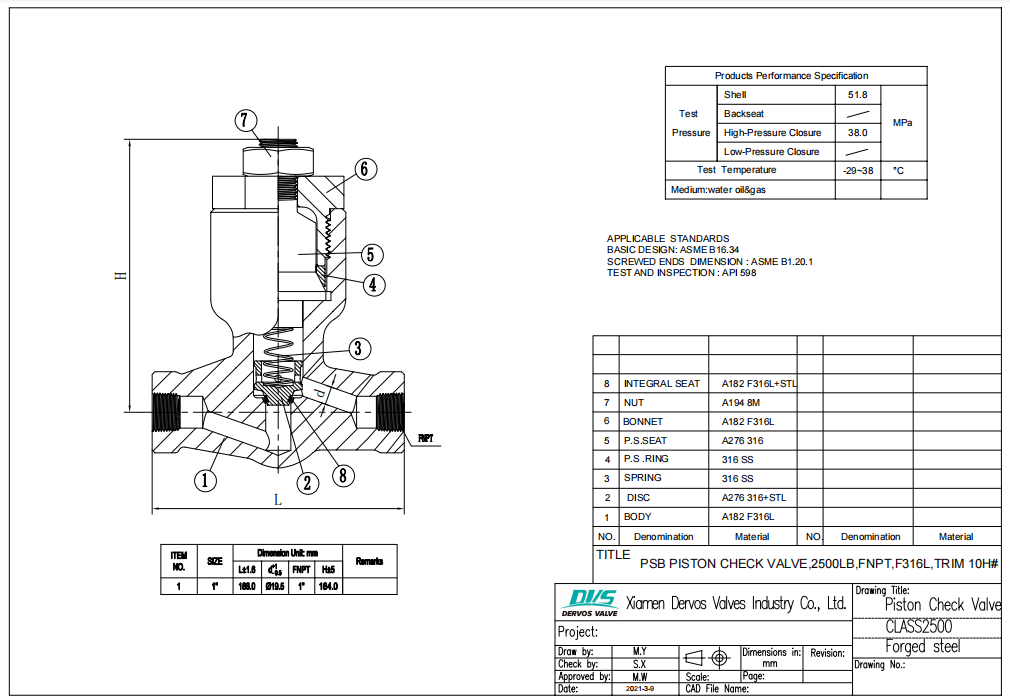
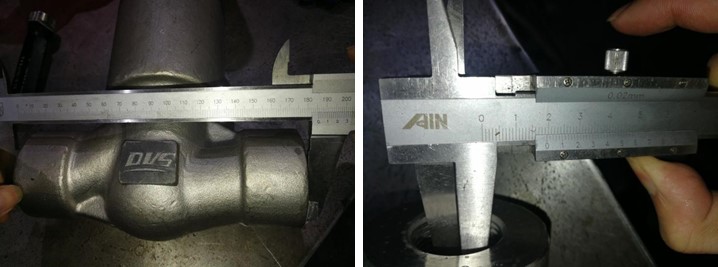
Dimension Checking
Pressure Testing
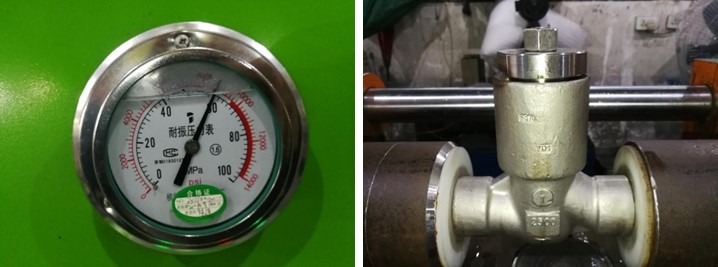
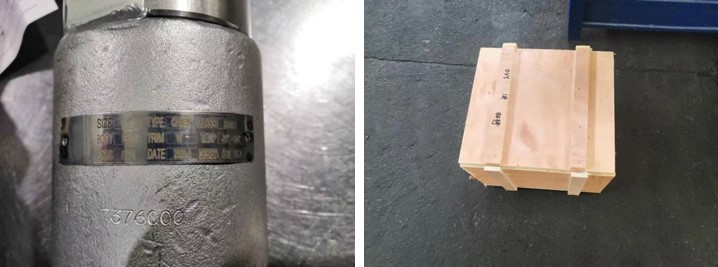
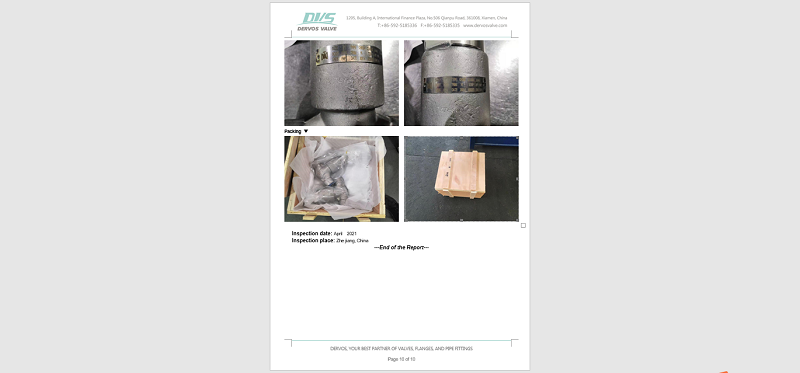
Nameplate & Packing
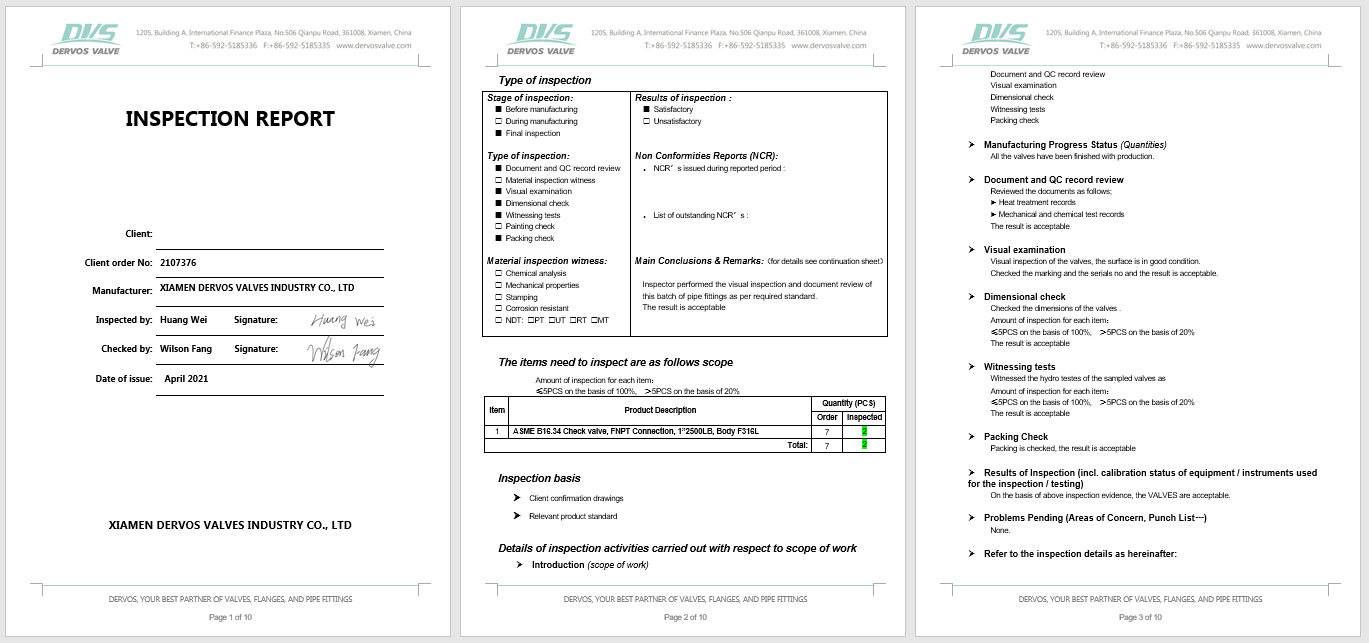
Inspection report
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
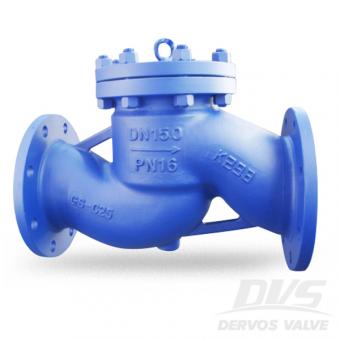
The cast steel lift non return check valve is designed with piston type disc, bolted bonnet, and PN16 RF flange. The spring loaded check valve conforms to DIN 3356. Quick Detail Type Check Valve ( Non-return Valve) Nominal Diameter DN 150 NominalPressure PN 16 Construction Lift Type / Piston Type, Bolted Bonnet Connection Flanged Connection Design & Manufacture DIN 3356 End to End EN 558 Connection EN 1092 Test & Inspection EN 12266 Body Material Carbon Steel GS C25 Media W.O.G. Product Range Body material: CS, SS, Alloy Steel, CI, Bronze, Brass Size Range: 2”~12” (DN50~DN300) End Type: Butt Weld, Socket Weld, Flanged, Screwed Pressure Range: 150lbs~2500lbs (PN16~PN420) Temperature Range: -46℃~ +425℃ Related Knowledge What is a piston check valve? Usually, we have swing type check valve and lift type check valve. A piston check valve and ball check valve both belong to lift type check valve. In a lot of cases, a piston check valve use spring to retain the disc in closed position. The structure of a piston check valve is very similar to the globe valve just without manual operation. Due to its piston type disc and superior leak tight characteristic, the piston check valves are suitable for small size and high pressure conditions.
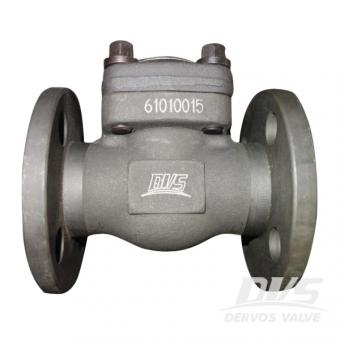
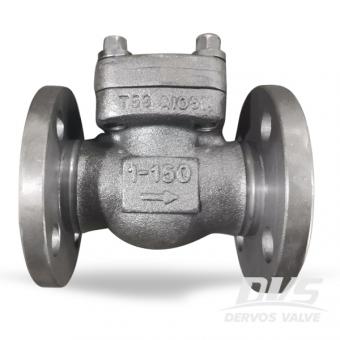
The forged steel lift check valve is designed with class 150 pressure and 1 inch nominal size according to standard API 602. We also call it as piston check valve. Quick Detail Type Check Valve Size 1'' DesignPressure 150LB Construction Lift Type, Piston Type Connection RF Flange Design & Manufacture API 602 End to End ASME B16.10 Connection ASME B16.5 Pressure & Temp ASME B16.34 Test & Inspection API 598 Body Material ASTM A105N Trim Material Trim 5 Temp Range -29℃~+425℃ Media W.O.G. Dimension Checking Pressure Tesing Packing
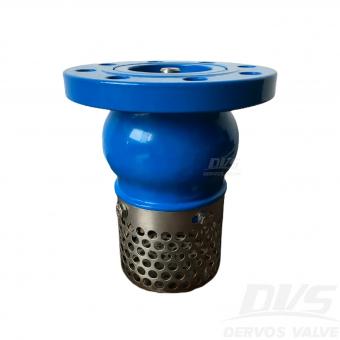
The 2 inch 150LB foot valve is made of stainless steel.
Due to its simple flow efficient and virtually maintenance-free design, thestainless steel ball checkvalve is commonly specified and used in submersible waste water lift stations.
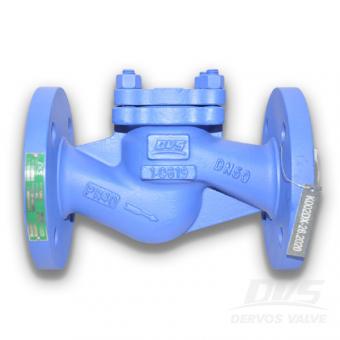
This spring loaded check valve, made according to DIN3840, requires no gravity or backflow pressure to work or actuate.It’s body material 1.0619 enable the valve to work under great heat and It’s spring can accommodate a wide range of temperature, too.
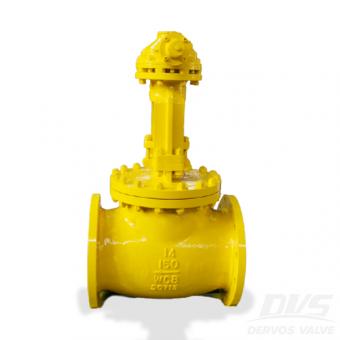
Chinese Valve manufacturer Dervos supplies Check Valve that featured with through conduit, plug type disc and replaceable seat. Expect these 14 inch 150LB check valve, other types valves of different materials, sizes are also available.
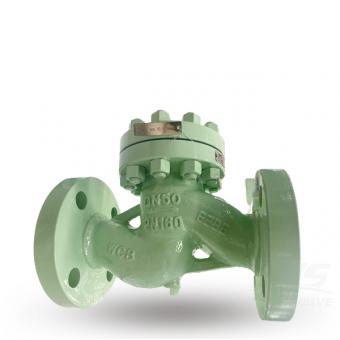
The DN50 PN160 spring loaded lift check valve, made of Cast Steel, is powered by flow and differential pressure with assistance from spring pressure. And it requests no human intervention is required to function, easy to use.
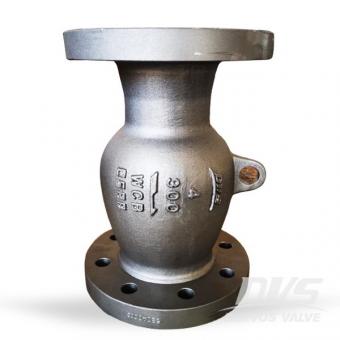
The stainless steel non return valve features in non slam type disc, INCONEL X750 spring, WCB valve body. This valve owns an excellent dynamic performance and minimizes vibrations and noise.
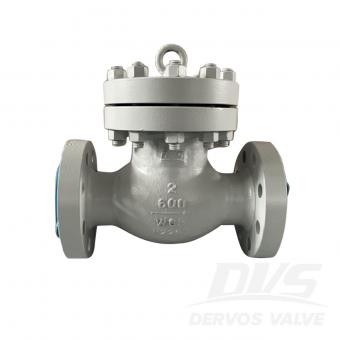
2" 600LB check valve is made according to BS1868 standard. The valve body is made of A216 WCB. It has the structural characteristics of lifting type, bolt cover and body valve seat. Its connection mode is RF.
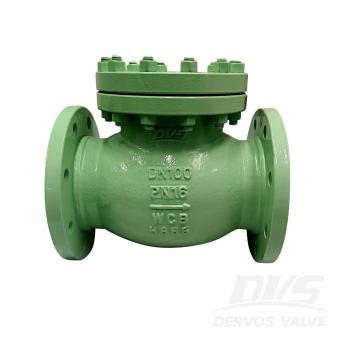
DN100 PN16 check valve is made according to EN12516-1 standard. The valve body is made of ASTM A216 WCB+STL. It has the structural characteristics of lifting type with spring. Its connection mode is EN1092-1 B.
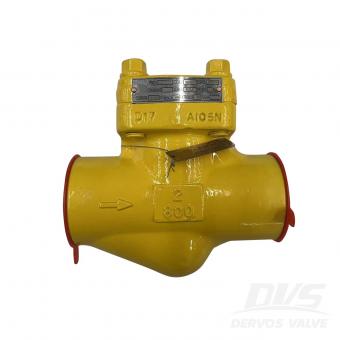
2" 800LB lift check valve is made according to API 602 standard. The valve body is made of ASTM A105N+STL. It has the structural characteristics of lift type. Its connection mode is SW.

DN80 PN16 lift check valve is made according to DIN 3356 and BS 1873 standard. The valve body is made of ASTM A216 WCB. It has the structural characteristics of lift type with spring. Its connection mode is EN1092-1 B.
Copyright © 2015-2026 DERVOS VALVE CO.,LTD.All Rights Reserved Blog / Sitemap / XML / Privacy Policy